

The biggest value of AI in quality management may not be writing reports faster. It may be finding the flaws in our own analysis.
That is the main lesson from my test: what convinced me were not the finished drafts, but the moments when the AI exposed a gap, a contradiction or a conclusion drawn too quickly.
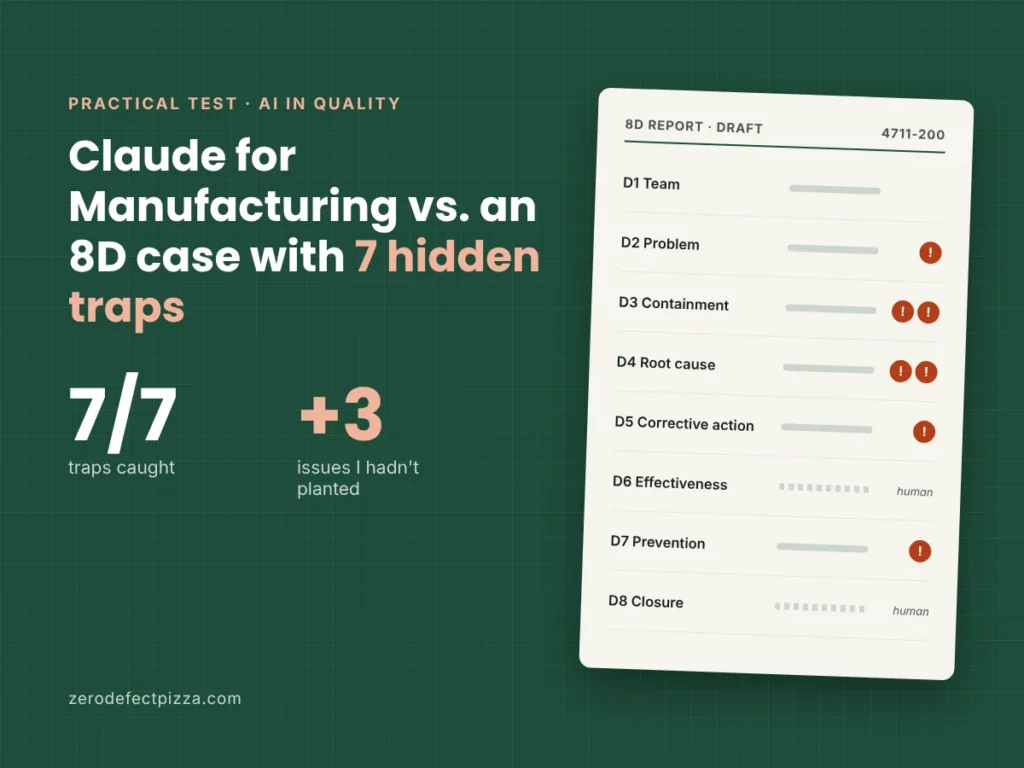
I ran Anthropic's new Claude for Manufacturing plugin through a full 8D case with seven hidden traps. It caught all seven and found three more problems I had not planted as traps. The quality logic is stricter than many 8D reports I have reviewed in supplier quality. Customer-specific 8D formats, FMEA feedback and approval packages are not covered out of the box.
The case ran in a fictional plant with fictional data. Claude generated the data set and ran the chain in one session. That makes it a function test, not a blind test.
What Claude for Manufacturing is
A plugin for Claude, released by Anthropic on 12 November 2026. It is not a separate product and needs a Team or Enterprise plan.
| Part | What it contains |
|---|---|
| Skills | 17, across sales, quality, operations, supply chain, design and setup; 4 of them for quality |
| Connectors | Microsoft 365, Oracle NetSuite, Infor M3, Autodesk Fusion; other systems through a custom-connector skill or scheduled file exports |
| Approval gates | Nothing is sent, applied or written to a system without an explicit yes from a named person |
| Status | A reference implementation, “not actively maintained” according to its README |
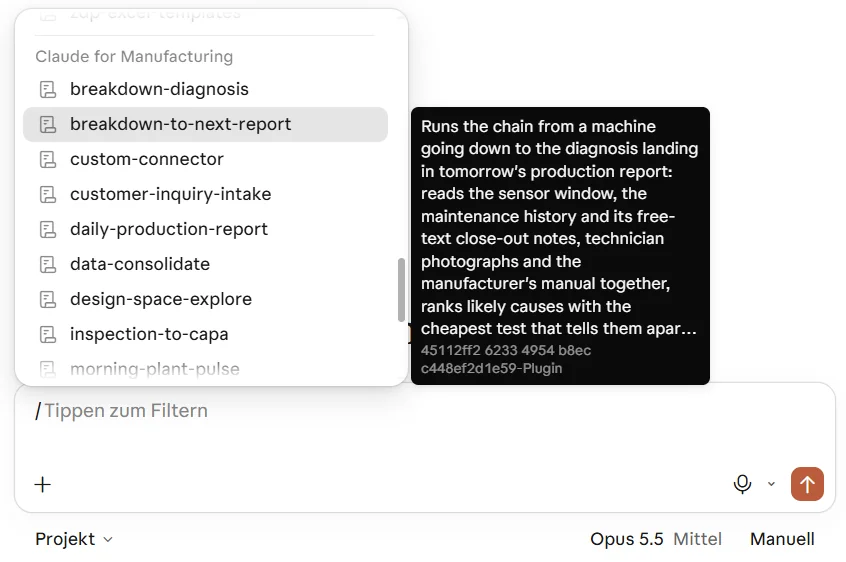
What a skill is: a written work instruction for Claude, much like a standard operating procedure. It defines the sequence, the rules, the edge cases and the approvals. The model brings the intelligence; the skill decides how it works.
The four quality skills
Two skills do the work, two chain them together. All four share two rules: compute, don't eyeball and rank, don't conclude.
| Skill | What it does | Rule that stood out |
|---|---|---|
ncr-writeup | Writes the nonconformance: what was found, against which requirement, how many parts, where they are | No cited requirement, no NCR. “Not checked” is never written as zero |
root-cause-capa | Puts measurements, sensor and maintenance data on one verified timeline, ranks causal chains, drafts the 8D | Evidence for and against every link; D6 and D8 stay empty |
inspection-to-capa | Chains the two, up to a redacted customer version | Two approval gates; a recurrence is never redacted |
supplier-escape-to-alternate-source | From a supplier-caused defect to an RFQ for an alternate source | Blaming a supplier needs its own approval; a tie means no blame |
The test setup
A classic customer escape: a bore undersize on a critical characteristic, with parts already at the customer.
| Element | Test data (all fictional) |
|---|---|
| Plant | Musterwerk GmbH, a fictional pump-component supplier; one site, three shifts |
| Part and characteristic | Valve housing 4711-200 rev C, bore Ø 12.000 +0.050/0, critical characteristic (CC) |
| Production | Three work orders on one machining centre; two from raw-material lot CH-2311, one from CH-2310 |
| Inspection data | 57 sampled measurements; the CH-2311 runs drift into undersize |
| Material certificates | CH-2311 at 103 HB against a spec of 75–95 HB |
| Where the parts are | 500 at the customer, 120 in transit, 280 in stock, 40 at the machine |
| Customer agreement | Notification within 24 hours; 8D within 10 working days for critical characteristics |
| History | A closed 8D on the same defect from March, plus a mislabelled old NCR |
Results: seven traps, seven caught
| Trap | What a weak investigation does | What the plugin did |
|---|---|---|
| Recurrence after a closed 8D | Treats it as a new case | Flagged “recurrence, previous fix failed”; D7 explains why the old fix did not hold |
| Parts at the customer | Notifies when the 8D is done | Drafted the notification immediately, deadline taken from the quality agreement |
| Unknown whether parts are installed | Leaves the location out | Listed it as “not checked”, never as zero |
| Material lot above hardness spec | Blames tool wear again | Found it through lot clustering: 10 of 37 samples out on CH-2311, 0 of 20 on CH-2310 |
| Clocks that do not line up | Matches events by eye | Refused to correlate across the unverified clock and said what still holds |
| Night shift looks guilty | Points at the operator | Called it small numbers at the end of each run, not a people problem |
| Mislabelled old NCR | Counts it as history | Excluded it: the work order belongs to a different part |
Every figure came from code over the data, with a figures block showing the filter behind each number.
Three findings I had not planted as traps
- A detection gap. Four readings below tolerance were recorded on 11 and 12 November, and the work order still shipped on 13 November. The 8D therefore splits D4 into occurrence and non-detection, and D5 adds a control chart with a stop rule.
- A hard stop in the supplier chain. There was no drawing and no revision for the raw part, and the supplier specification carried no index. The plugin refused to build an RFQ on an unverified revision and flagged the real risk first: the supplier who caused the defect is the only approved one.
- A control chart set too tight. In the simulated follow-up production, the new stop rule fired five times with zero bad parts. The limits had been computed from one short run; they were checked statistically and recalculated from 60 values.
Nobody set these up as traps; Claude spotted them on its own from the data and the rules in the skills. That is what makes the test interesting.
The 8D, the gates and the customer version
The chain stops at three gates and says where it stopped. In the test it paused twice for my confirmation and once at a hard stop.
The 8D followed the plant's own template. D1 to D5 and D7 were drafted from the evidence. Every D5 action names the link in the causal chain it breaks; 100% inspection was moved out of D5 and labelled “improvement, not corrective action”. D7 explained why the March fix failed: the earlier lot was also above hardness spec, and nobody looked.
The customer version was produced as a redaction diff: supplier name, operator IDs and maintenance orders out; the recurrence stays in. The quality owner approves the diff, not just the clean document.
Limits
- Function test, not blind test. Claude built the data and ran the chain in the same session. A real test needs a case whose answer the system does not know.
- Not ready for customer-specific quality rules out of the box. Customer 8D formats, FMEA and control-plan feedback, approval packages and customer portal formats are not included. The plant's own template can be loaded, and the skills can be adapted.
- Data quality decides. Old 8Ds that sit in no connected system are not found. The recurrence check is a search, not learning.
- Cloud and licence. It runs on Anthropic's cloud and needs a Team or Enterprise plan. Commercial plans are not used for model training by default; retention controls are an Enterprise feature.
- Reference version. Anthropic does not promise maintenance. Skills may change; this report reflects the state of 15 November 2026.
- Competence. If the AI always ranks the causes, teams may stop practising problem solving.
Who it is for
| Fit | Who | Why |
|---|---|---|
| Good fit | Mid-sized manufacturers without deep CAQ or an AI team, running Microsoft 365, NetSuite or Infor | Fast start into clean NCR and 8D practice; the gates enforce human sign-off |
| With adaptation | Suppliers with customer-specific quality rules | Add skills for their 8D format, FMEA and control-plan feedback, approval packages |
| Not yet | Multi-tier supply-chain steering; plants with a no-cloud policy | No n-tier view; cloud only |
For managing directors, three questions decide whether to start: which data classes may go to the cloud, which systems you are willing to connect, and who in your quality team owns the approvals. Start with one product line and one recent, closed 8D you know well. Run it again with the plugin and compare.
My verdict
Not a substitute for problem-solving skills, but a serious sparring partner.
For years we have asked how AI can help quality engineers write reports faster. Perhaps that is the wrong question. What the test showed above all is what a team easily overlooks: a detection gap, a missing revision, a control chart set too tight.
The AI drafts. People check the evidence, decide and prove effectiveness.
In pizza terms: Claude puts on the toppings. Whether the base is done is the pizzaiolo's call.
Get the test package — free
Fictional data set, NCR, internal 8D, customer 8D and redaction diff — everything from this test, in English (translated from the German original run). Unlock once with your email and you also get access to all ZeroDefectPizza Excel templates.
Unlock with email & downloadSources
- Anthropic: Introducing Claude for Manufacturing
- Plugin skill files: anthropics/claude-plugins-official
- Anthropic Privacy Center: data processor or controller?
ZeroDefectPizza is not affiliated with Anthropic. All plant, part, supplier and customer names in the test are fictional.